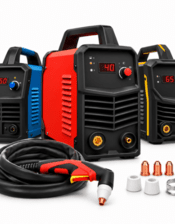
Plasma cutting machines cut electrically conductive metals using a high-temperature plasma jet. They are used for mild steel, stainless steel, aluminium and other compatible metals in fabrication workshops, automotive repair, construction and industrial metalworking.
Irankistai.lt offers 220–230 V and 380–400 V plasma cutters, including KRAFT&DELE KD1848 and KD3424, Sherman CUTTER 50 and CUTTER 70, PULI CUT60L and CUT80A, and YOULI YLCUT60. Models differ in cutting current, duty cycle, compressed-air requirements and manufacturer-declared cutting capacity. Always check individual product specifications.
230 V plasma cutting machines can suit workshops with a sufficiently rated single-phase electrical supply. Examples include KRAFT&DELE KD1848 and KD3424, Sherman CUTTER 50 and PULI CUT60L. Three-phase 380–400 V models include Sherman CUTTER 70, PULI CUT80A and YOULI YLCUT60. Three-phase input does not automatically mean higher cutting performance; compare the full technical specifications.
| Model | Input voltage | Catalogue cutting current | Declared maximum thickness |
|---|---|---|---|
| KRAFT&DELE KD1848 | 230 V | 60 A | Check product listing |
| KRAFT&DELE KD3424 | 230 V | 75 A | 25 mm |
| Sherman CUTTER 50 | 230 V | 45 A | 12 mm |
| Sherman CUTTER 70 | 400 V | 65 A | 23 mm |
| PULI CUT60L | 220 V | 20–60 A | 20 mm |
| PULI CUT80A | 380 V | 20–80 A | 30 mm |
| YOULI YLCUT60 | 380 V | 20–60 A | 18 mm |
Figures reflect catalogue specifications. Manufacturer-declared maximum thickness is not a guarantee of clean-cut performance under every operating condition.
Actual cutting performance depends on the metal, current, air supply, travel speed and torch condition. Maximum stated thickness may describe a severance limit rather than the best setting for everyday production. For frequent cutting of thicker material, allow sufficient current and duty-cycle capacity.
Many air plasma cutters need an external compressor. Continuous delivered airflow matters as much as maximum pressure. The catalogue lists air requirements of 200 l/min for Sherman CUTTER 50 and PULI CUT60L, 250 l/min for KRAFT&DELE KD3424 and Sherman CUTTER 70, and 120 l/min for YOULI YLCUT60. Match the compressor to the individual machine's airflow and operating-pressure requirements.
Good edge quality depends on appropriate current, steady torch movement, correct torch-to-work distance and clean, dry air. Worn electrodes and nozzles can reduce arc stability and cutting quality. Select replacement consumables according to the exact torch model and manufacturer compatibility guidance.
Plasma cutting generates intense light, hot particles, fumes and noise. Use suitable eye and face protection, gloves, protective clothing and effective fume extraction. Check electrical connections, grounding, compressed-air supply and fire precautions. Follow the equipment manufacturer's instructions.
Yes, provided the machine and settings suit the electrically conductive aluminium workpiece and its thickness.
It can be if its cutting current, duty cycle, electrical supply and air system meet the intended workload.
These are manufacturer model or series designations and may not exactly match the actual rated cutting current. Check the technical specifications.
Many air plasma cutters require a compressed-air source with sufficient pressure and continuous airflow.
Not necessarily. The declared maximum may be a severance limit, while a lower thickness is recommended for consistent clean cuts.
Yes, when a suitable machine and settings are used for the material thickness.